Project Overview
Sunoco Chemical closed its aniline plant in 2001 due to changing market conditions. The plant was located within a larger chemical facility that continued to operate several other process units. As part of a broader initiative to exit non-core businesses, Sunoco prepared the site for sale and wanted the inactive areas removed before marketing the property.
The removal scope included the former aniline plant along with a thermal oxidizer area, boiler area, exhaust stack area, and boneyard. Phoenix Equipment purchased the redundant assets and performed the dismantlement and environmental work at no cost to Sunoco. The approximately $2.5 million project was completed over roughly seven months.
The Challenge
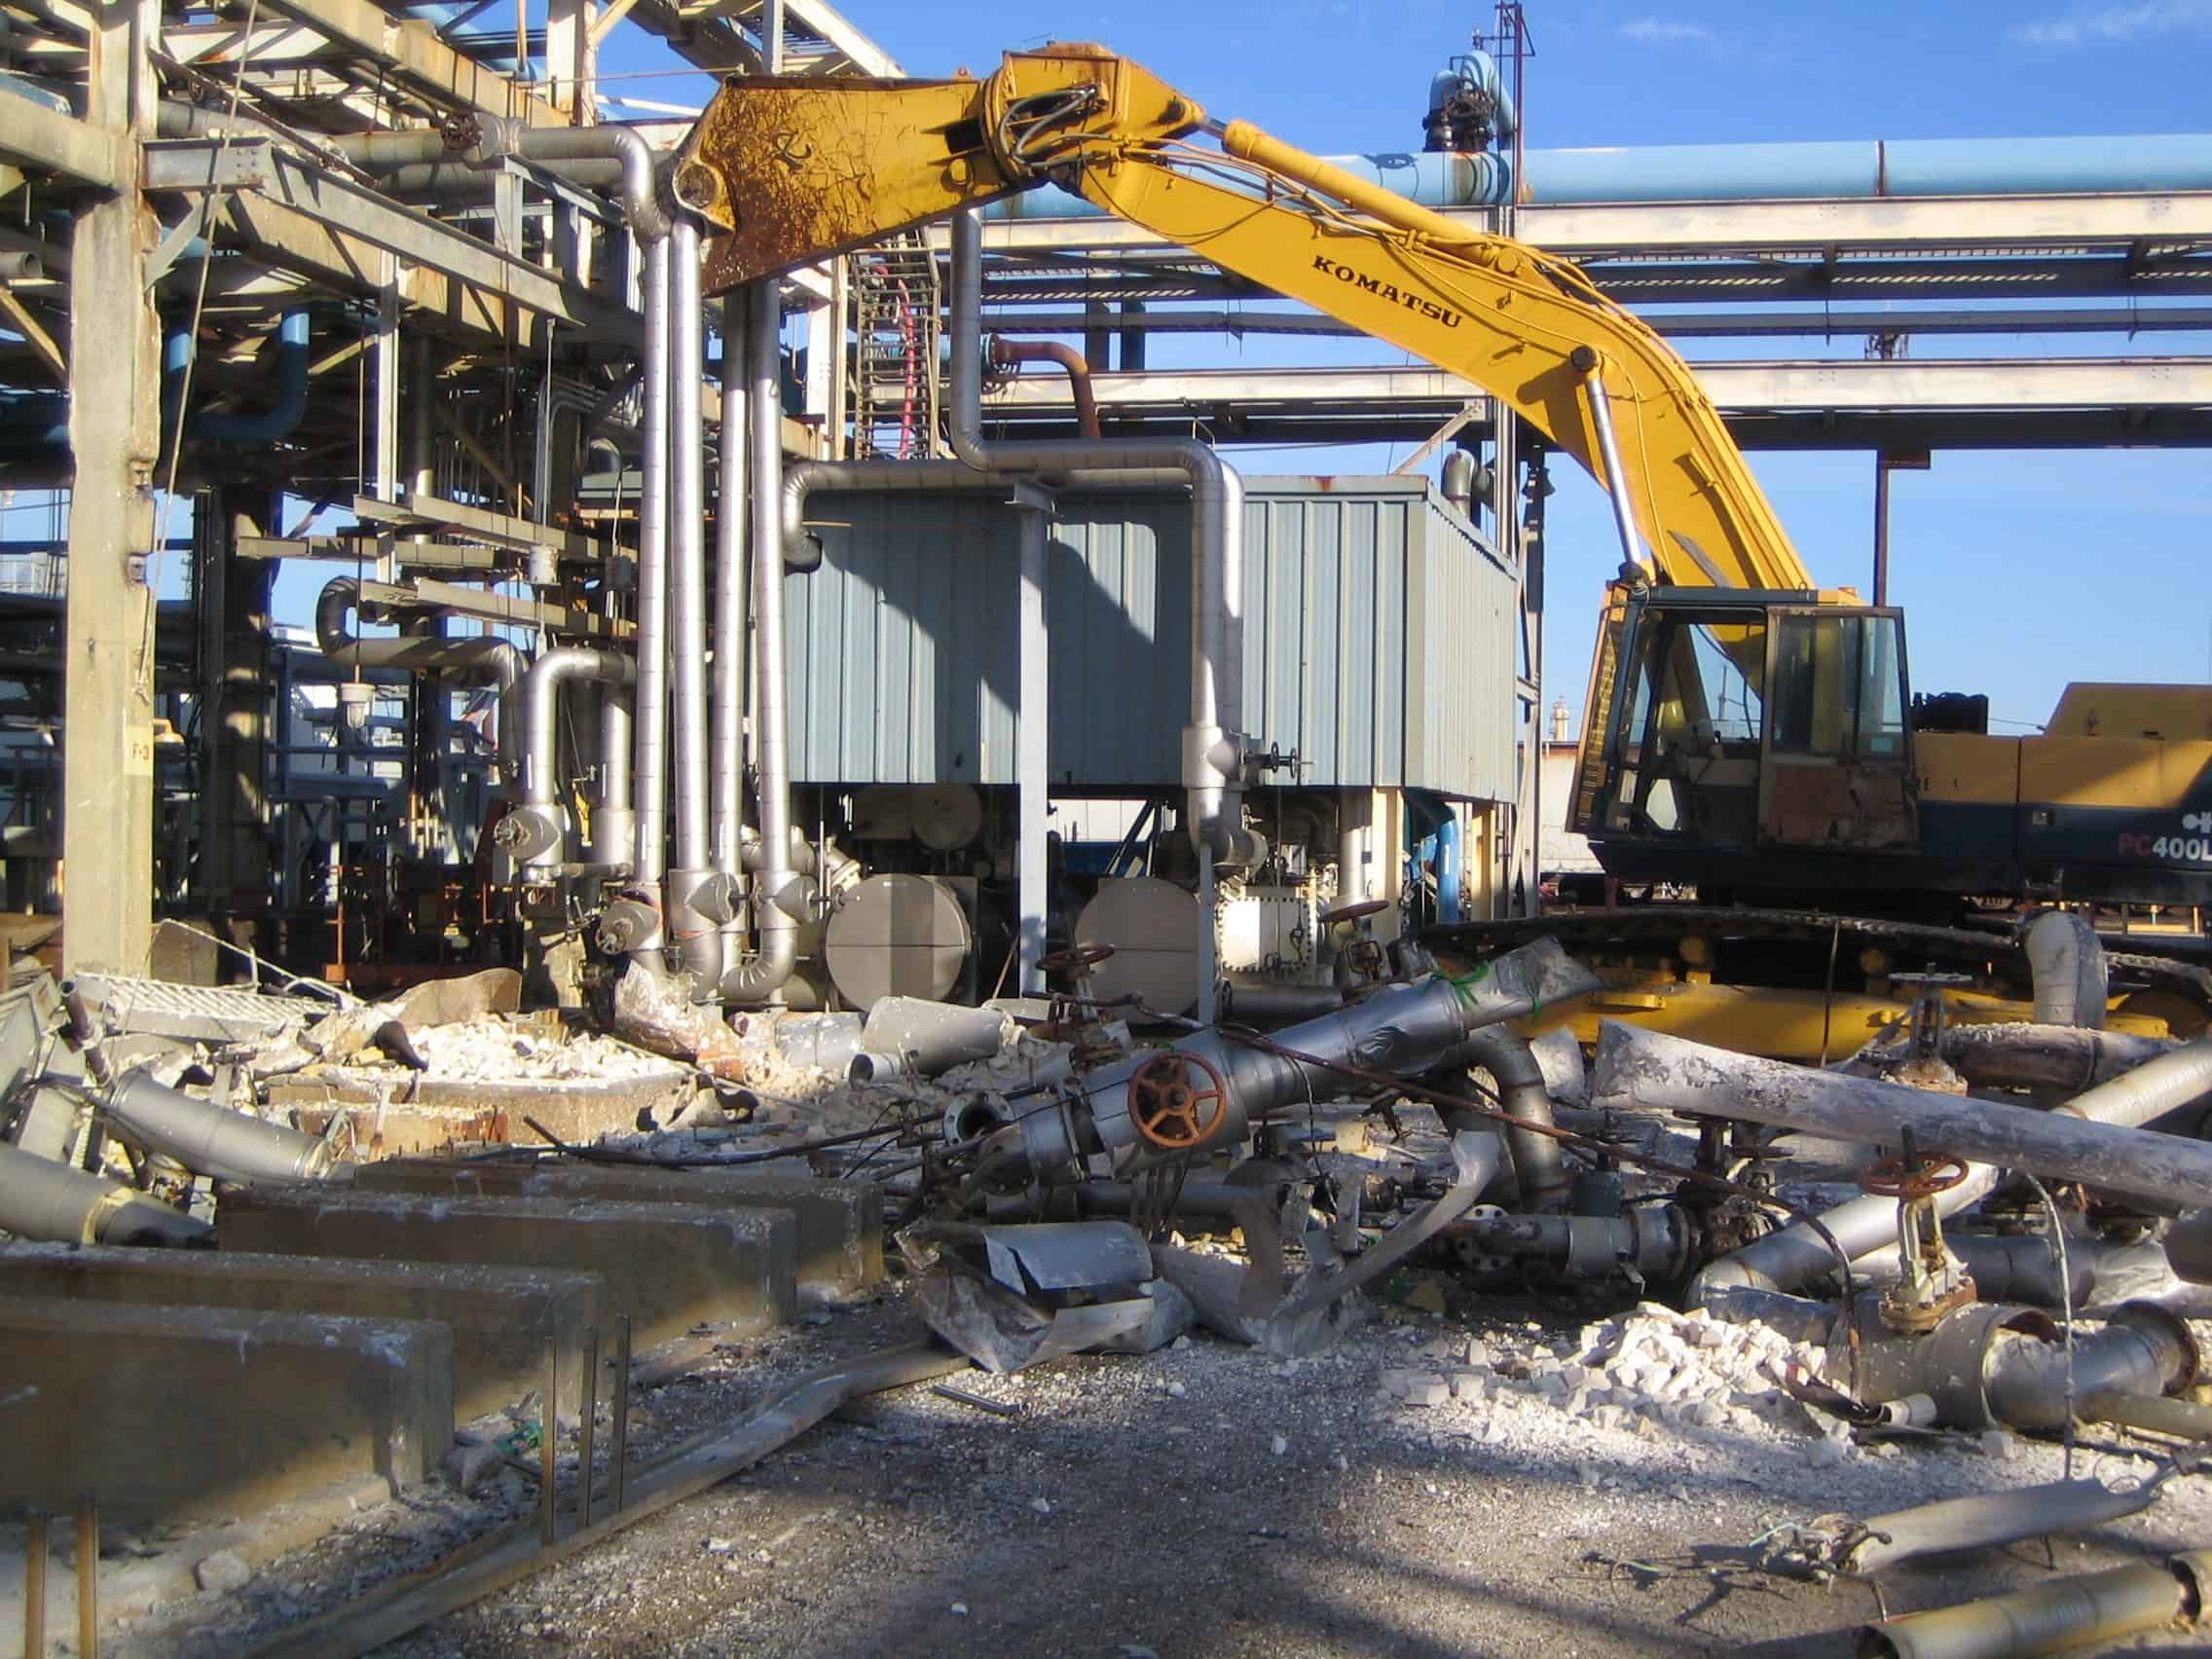
Sunoco needed to remove inactive process areas from within an operating chemical facility while managing uncertain residual conditions from a plant that had been shut down for more than a decade. The aniline plant itself covered more than 80,000 square feet, and historical records suggested that alumina catalyst could remain in two reactors while several heat exchangers might still contain residue.
Other parts of the site presented their own constraints. Large bullet tanks sat in a diked area surrounded by soft ground, a 150-foot column had to be removed near active pipe bridges and tank storage, and the thermal oxidizer was located beneath a steel structure supporting active equipment and piping.
Asset Recovery & Equipment Resale
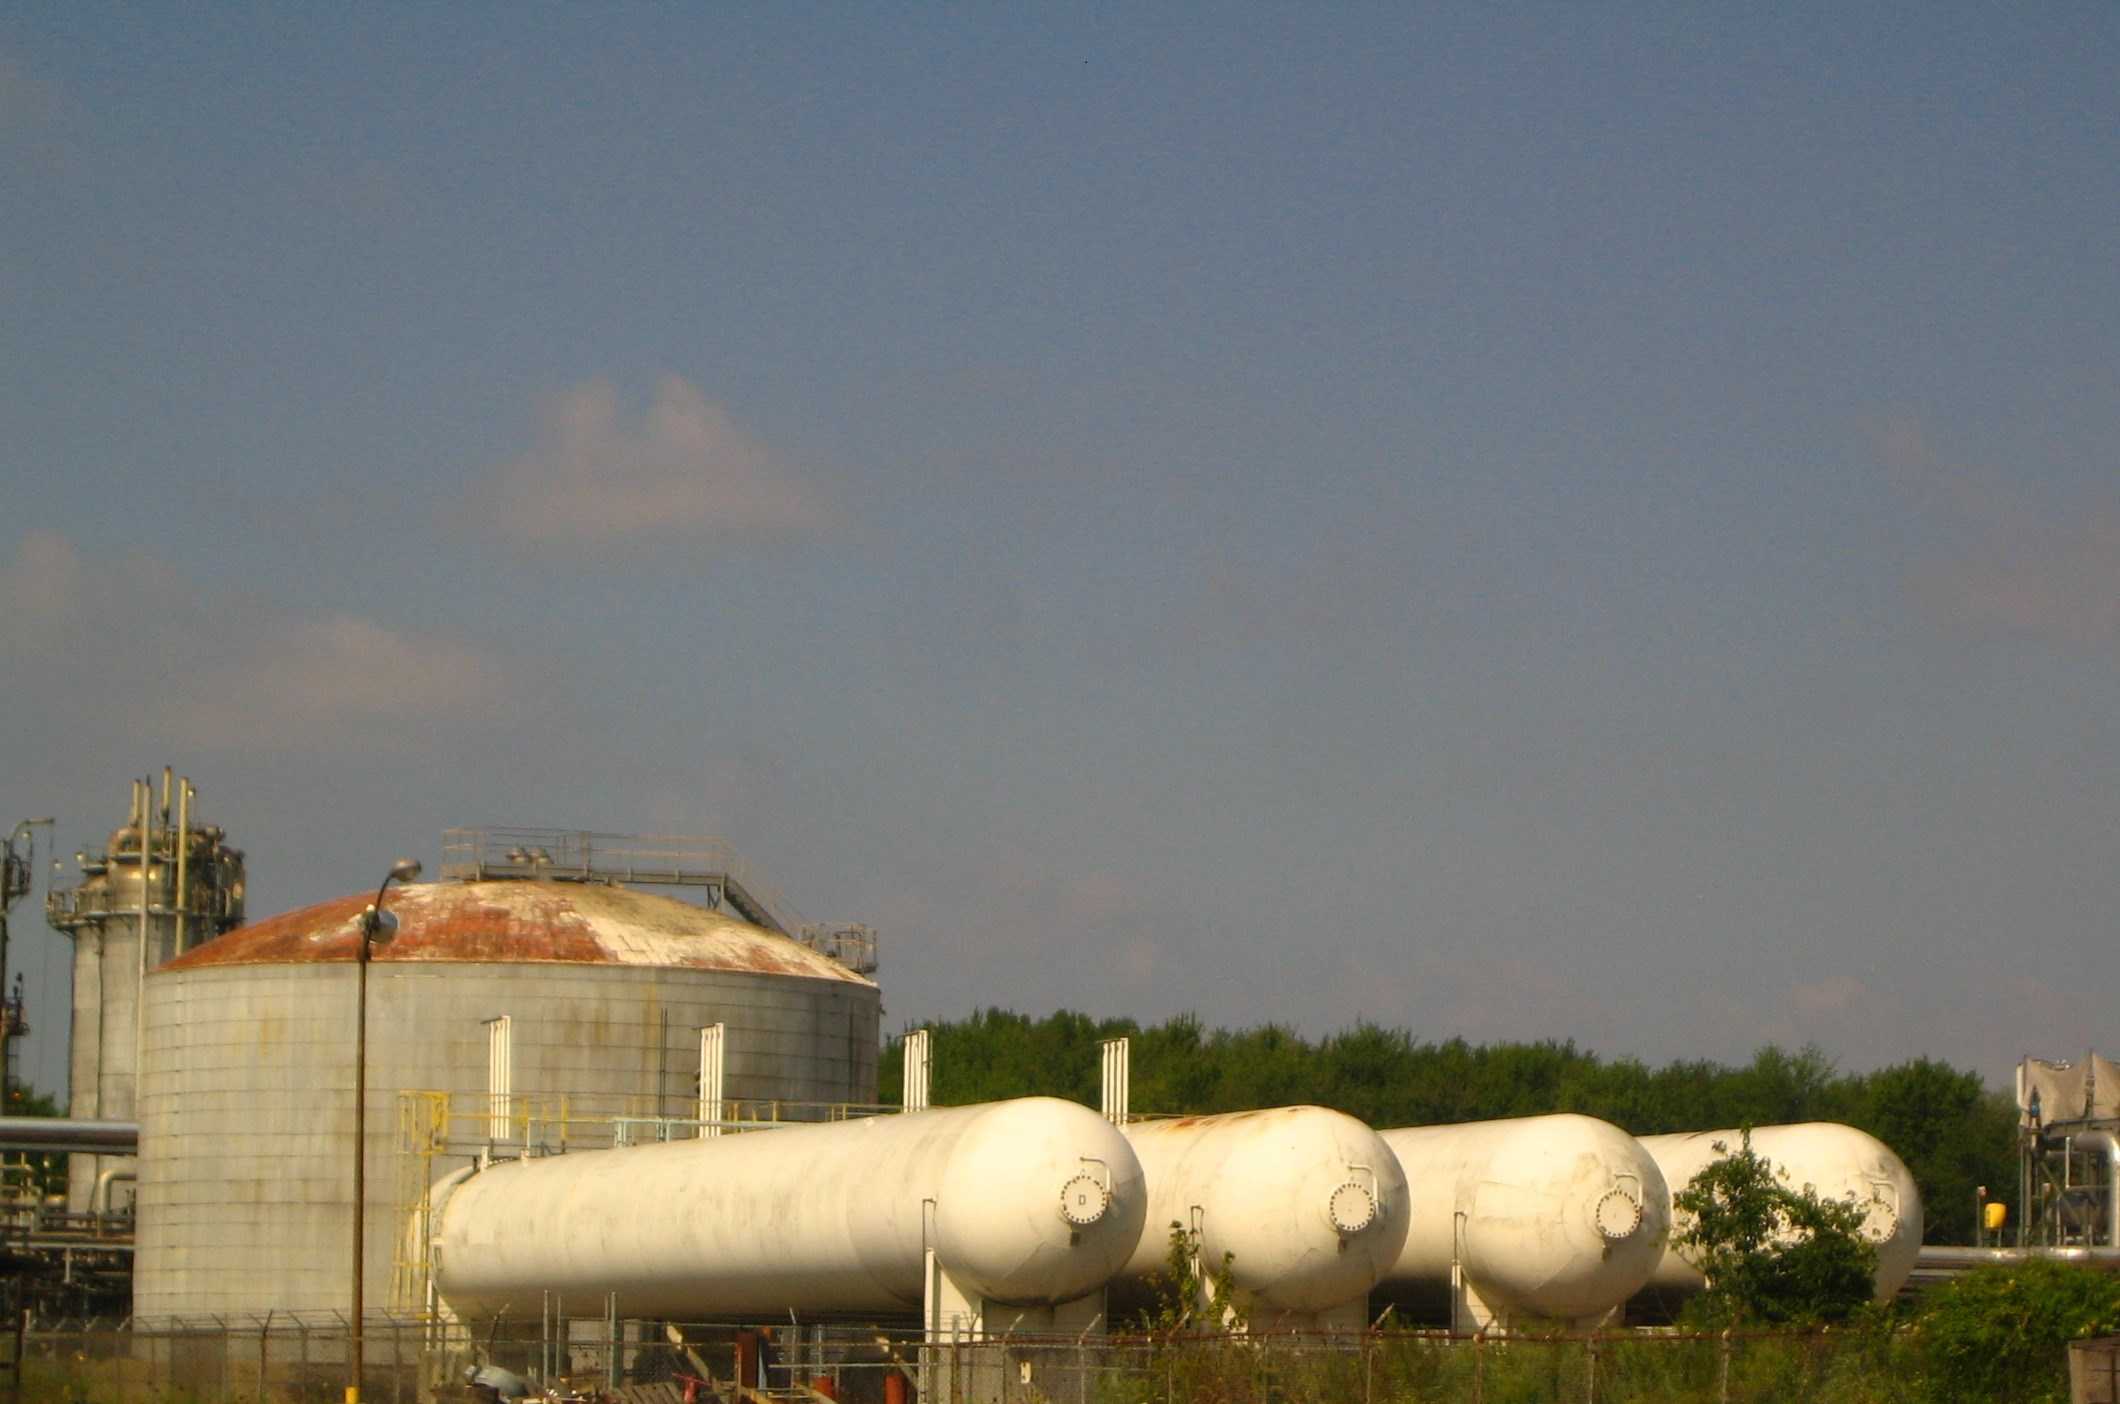
Phoenix’s ability to recover value above scrap supported the economics of the project. More than 45 pieces of process equipment were safely dismantled and rigged out for resale, including:
- 4 × 90,000-gallon bullet tanks, rated 250 psi
- Multi-stage Pfaudler wiped film evaporator system
- Ammonia recovery system
- Riley Stoker boiler system
- Callidus Technologies thermal oxidizer system
- 2 stainless steel scrubbing systems
- Stainless steel and carbon steel packed and tray columns
- 25+ stainless steel and carbon steel shell-and-tube heat exchangers
Phoenix also recovered more than 1,000,000 pounds of non-ferrous material and more than 2,500 tons of carbon steel through recycling.
The resale value of the process equipment and recovered metals allowed Phoenix to pay Sunoco for the assets while completing the dismantlement and environmental scope at no cost to the owner.
Environmental Management & Equipment Cleaning
Because Phoenix could not confirm the effectiveness of cleanup work performed more than ten years earlier, a dedicated equipment and piping cleanup area was established within the former aniline plant. Water was restored to the cleanup area and connected to an active chemical sewer in an adjacent operating section of the site.
Using appropriate PPE, crews performed line breaks at equipment connections and low points, then moved equipment and piping to the designated cleanup area as required. The two reactors were found to contain alumina catalyst. Phoenix tested the material and identified a recycler, avoiding the higher cost of landfill disposal.
Complex Rigging & Selective Dismantlement
Several major removal tasks required site-specific engineering. The four 90,000-gallon bullet tanks sat inside a diked area surrounded by soft ground, so Phoenix’s professional engineer designed a dunnage system that allowed the crane to be positioned close enough for safe lifting.
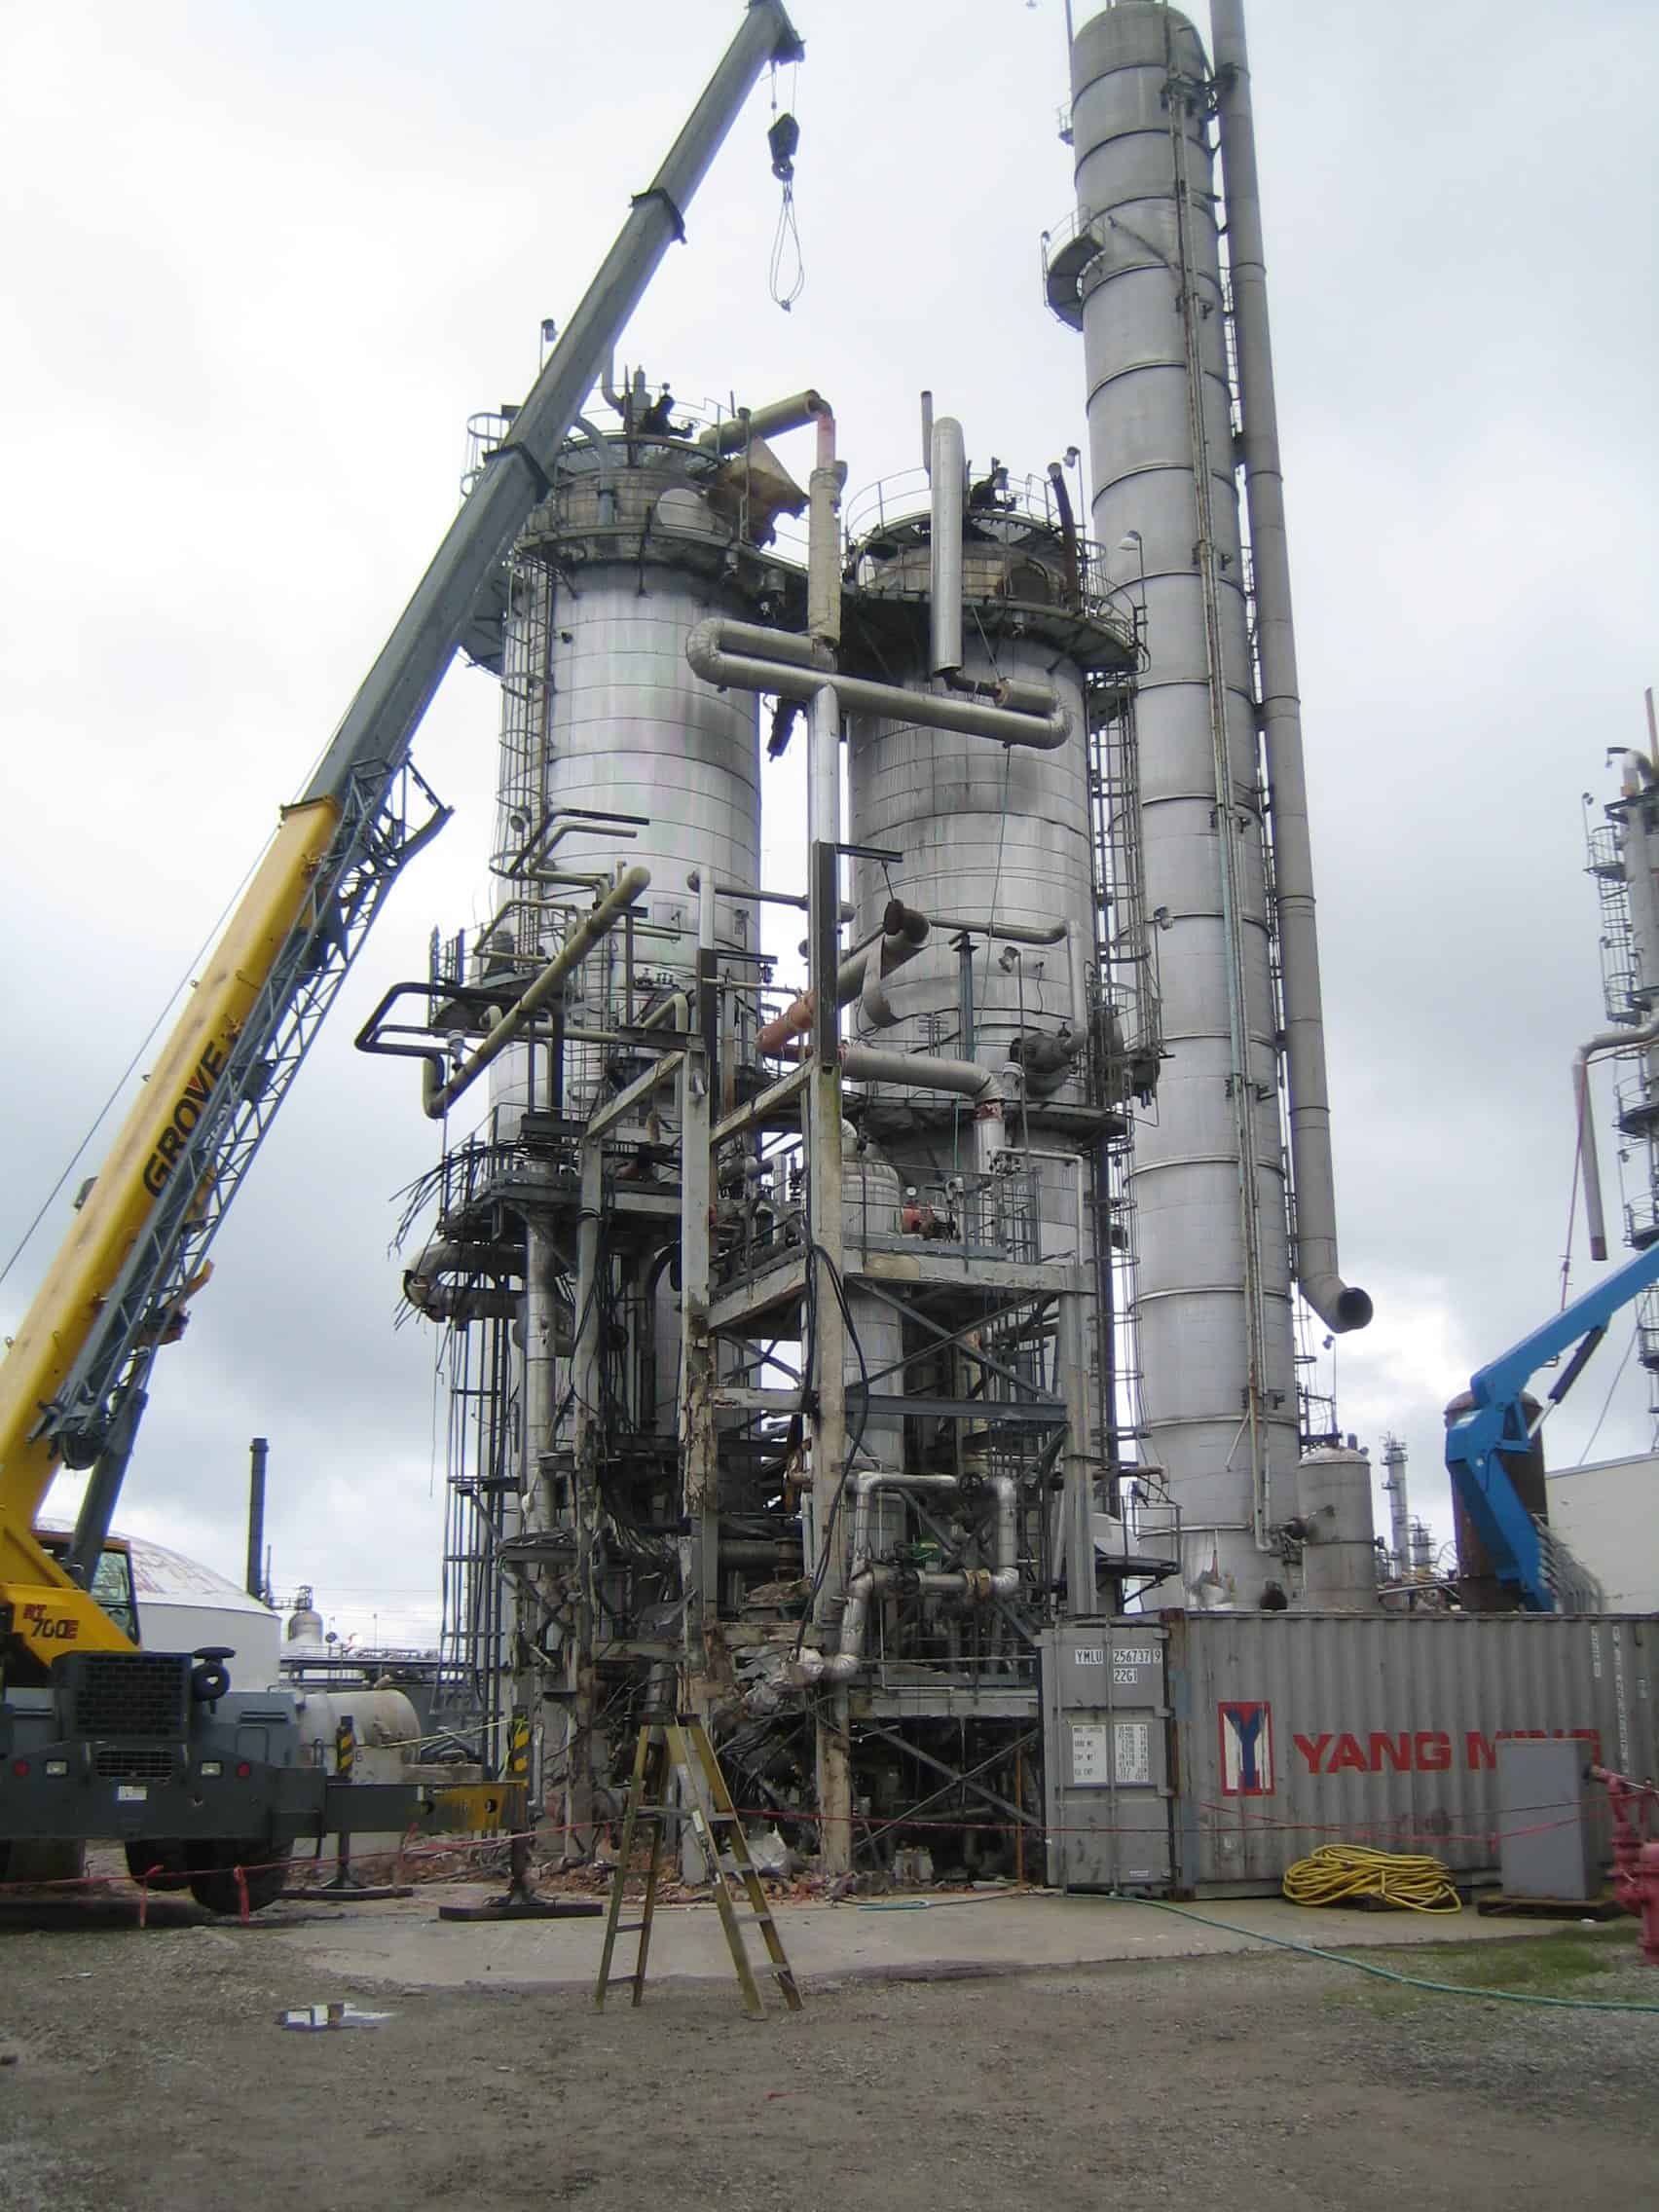
A 150-foot column in the boiler area stood within a congested zone bordered by elevated active pipe bridges and an operating tank storage area. Phoenix developed a spark-containment approach and dismantled the column in sections using a man-lift and heavy crane support.
The thermal oxidizer created another selective-removal challenge because it sat beneath a steel structure supporting active equipment and piping. Phoenix sectionalized and removed the oxidizer without disturbing the retained infrastructure above it.
Project Execution & Safety
A ten-person crew spent approximately seven months completing the project, coordinating rigging and demolition around active areas of the facility. The work included equipment and piping rinsing, catalyst recovery, equipment rigging, dismantlement, demolition, and scrap recycling, and was completed without injury or incident.
Project Highlights
- Client: Sunoco Chemical
- Facility: Aniline Plant and Associated Shutdown Areas
- Site Conditions: Inactive Process Areas Within an Operating Chemical Facility
- Primary Areas Removed: Aniline Plant, Thermal Oxidizer Area, Boiler Area, Exhaust Stack Area and Boneyard
- Aniline Plant Footprint: More Than 80,000 Square Feet
- Phoenix Scope: Plant Acquisition, Asset Recovery, Environmental Management, Equipment Cleaning, Rigging, Dismantlement, Demolition and Scrap Recycling
- Equipment Recovered: More Than 45 Pieces (See Liquidation)
- Major Equipment: 90,000-Gallon Bullet Tanks, Wiped Film Evaporator, Ammonia Recovery System, Boiler System, Thermal Oxidizer, Scrubbers, Columns and Heat Exchangers
- Non-Ferrous Material Recovered: More Than 1,000,000 Pounds
- Carbon Steel Recycled: More Than 2,500 Tons
- Environmental Work: Equipment and Piping Rinsing / Alumina Catalyst Testing and Recycling
- Major Execution Challenges: Soft-Ground Heavy Lifts / 150-Foot Column Removal / Selective Removal Around Active Infrastructure
- Project Duration: Approximately 7 Months
- Project Value: Approximately $2.5 Million
- Safety: Completed Without Injury or Incident
- Owner Outcome: Paid for Redundant Assets / Dismantlement and Environmental Work Completed at No Cost
Recovering Value While Clearing Inactive Process Areas
Phoenix used the resale value of the process equipment and recovered metals to offset a demanding dismantlement and environmental scope inside an operating chemical facility. Sunoco was paid for the redundant assets, avoided the cost of removal, and cleared inactive areas ahead of the broader site sale.